This phenomenon is known in the industry as “uncontrolled shrinkage.” Because the rotocasting process involves high-temperature molding and complex physical changes during cooling, its dimensional accuracy is much harder to control than that of Injection Molding. As a professional B2B toy factory supplier, MIHOX will provide an in-depth analysis from a technical perspective: How does vinyl shrinkage occur? And how does a professional factory use systematic engineering to control it at a micrometer level?
Part 1: Deep Dive into the Underlying Logic — Why Do Vinyl Toys Inevitably “Shrink”?
To solve the problem, we must first understand the physical properties of the material. The primary raw material for vinyl toys is PVC Plastisol, a liquid suspension system composed of PVC resin powder, plasticizers, stabilizers, and pigments.
1. The Thermodynamic Cycle: Volume Collapse from 200°C to Room Temperature
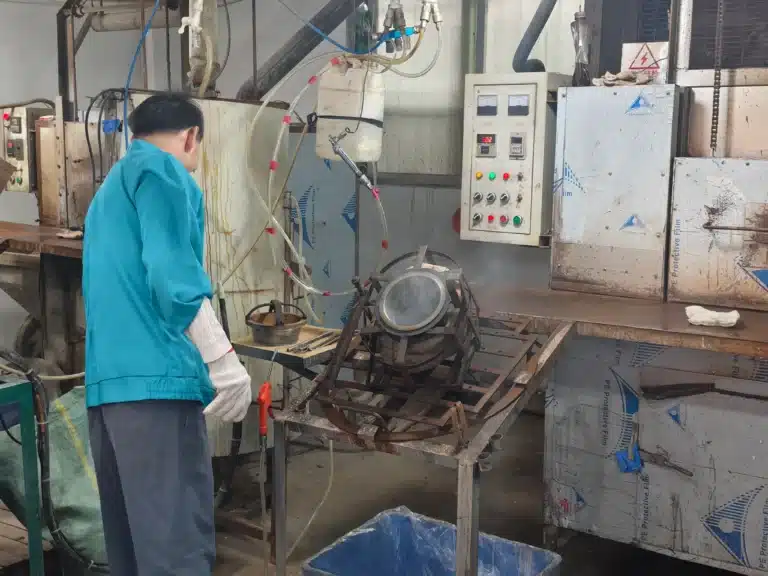
Inside the rotocasting machine, the mold is heated to 180°C–220°C. At this point, the liquid PVC adheres to the inner wall of the mold, undergoing “gelation” and “fusion” to form a dense solid film layer.
High-Temperature Expansion State: While inside the mold, the distance between molecules reaches its maximum due to thermal motion.
Cooling Contraction State: After the part is removed from the mold and the temperature drops, the molecular chains begin to realign and move closer together. This microscopic movement manifests macroscopically as a reduction in volume.
2. Difference Between Linear and Volumetric Shrinkage
The shrinkage of vinyl parts is not a simple proportional reduction. Since parts come in various shapes and have different stress points, shrinkage exhibits non-linear characteristics.
Centripetal Shrinkage: Spherical parts shrink toward the center, causing the diameter to decrease.
Stress-Induced Shrinkage: Irregular parts generate internal stress at turning points, leading to uneven contraction—the primary culprit behind assembly gaps.
Part 2: Root Cause Analysis — Five Dimensions Leading to Excessive Assembly Gaps
In MIHOX’s production practice, we have found that gap issues are usually caused by mismatches in the following five dimensions:
1. “Cooling Temperature Differences” Caused by Geometric Structure
In a complex figure, the torso usually has a larger internal space and cools slowly, while the arms and accessories are thinner and cool extremely fast.
The Result: The fast-cooling parts complete their shrinkage first, while the slow-cooling parts continue to shrink for several hours. If the wall thickness at the interface of these two parts is poorly designed, this time difference in contraction causes the originally matched “tenon-and-mortise” structure to deform and misalign.
2. “One-Size-Fits-All” Mold Compensation Coefficients
Ordinary factories often apply a uniform 2% shrinkage rate to enlarge mold dimensions during development.
The Truth: Different hardness levels of PVC and different part shapes result in actual shrinkage rates fluctuating between 1.5% and 2.8%. If the head requires 2.5% compensation while the body only needs 1.8%, using a uniform 2% will result in a head that is too small and a body that is too large, naturally creating a massive gap.
3. Variables in PVC Formula and Hardness
The content of plasticizers (such as DOP/DOTP) determines the product’s hardness (Shore A).
The Rule: Generally, the softer the material (the more plasticizer it contains), the higher the shrinkage rate. Many clients request both hard and soft versions from the same set of molds; under strict precision requirements, this is nearly impossible because one mold set can only correspond to one precise shrinkage formula.
4. Uniformity of Copper Mold Wall Thickness (Electroforming Defects)
Vinyl molds are mostly electroformed copper molds. If the current is not properly controlled during electroforming, the inner walls of the mold may vary in thickness, leading to deviations in heat conduction efficiency.
The Result: Uneven heat in the mold leads to inconsistent wall thickness in the product, which in turn triggers local shrinkage deviations.
5. Lack of Post-Process Setting Procedures
When a vinyl part first leaves the mold, it is in a “thermoplastic state.” Without professional setting jigs to hold its shape, the part may be affected by gravity while stacked, causing the interface to flatten slightly and turning a circular assembly point into an oval.
Part 3: MIHOX Engineering-Grade Solutions — How to Achieve “Zero-Gap” Perception?
To meet the B2B demand for high precision, MIHOX has established a control system combining digital simulation with physical intervention.
1. “Pre-Shrinkage Simulation” and “Joint Compensation” in the 3D Stage
During the modeling phase, our engineers do more than just draw; they perform physical simulations.
Dynamic Joint Design: We design the male part (plug) with a 0.5-degree taper and the female part (socket) with a deep-step joint. This allows for depth adjustment even if slight shrinkage occurs, hiding the gap from the exterior.
Wall Thickness Standardization: We strictly require consistent wall thickness at component interfaces (e.g., a uniform 3mm) to ensure synchronized contraction.
2. Master Wax Scaling
In the unique “mold seeding” process of rotocasting, we create wax masters that are slightly larger than the final product.
Precise Enlargement: MIHOX maintains a proprietary shrinkage database. We calculate enlargement ratios precise to two decimal places based on the specific grade of PVC plastisol being used.
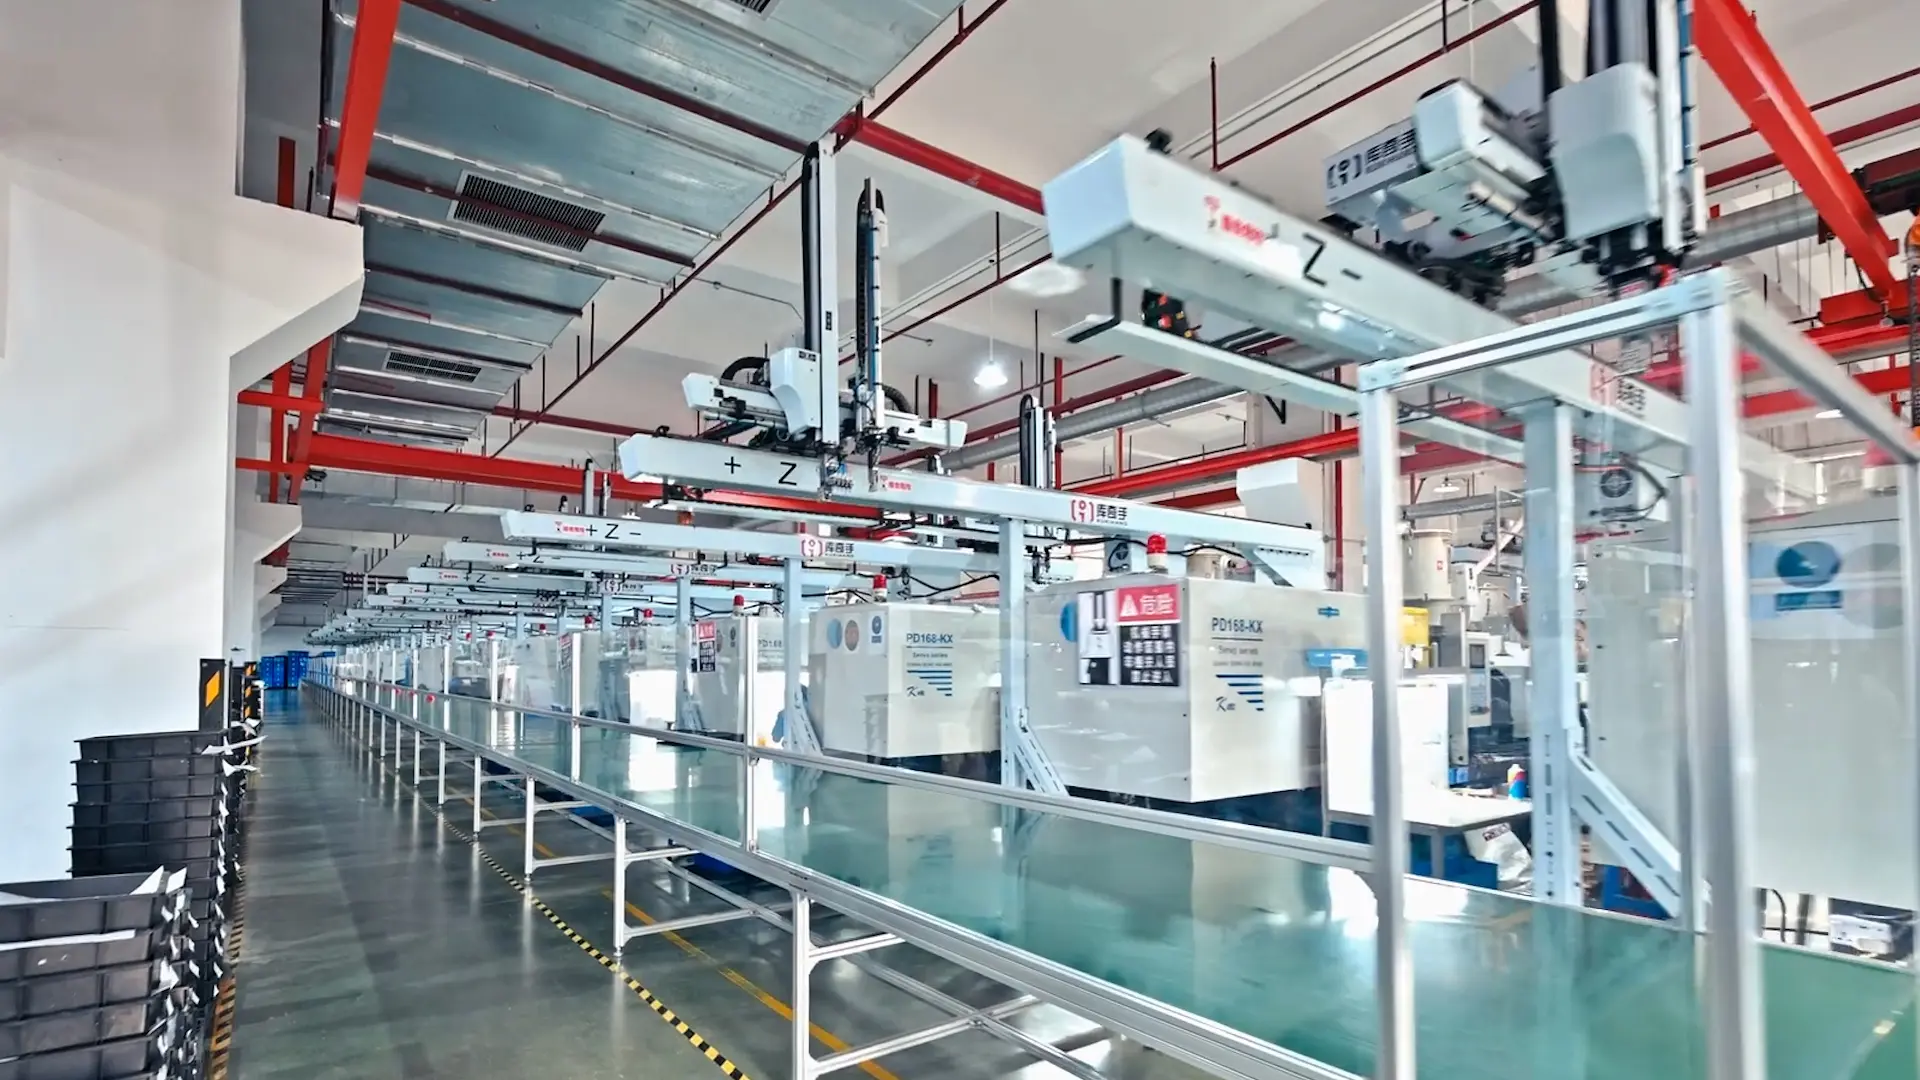
3. Digital Constant-Temperature Production Lines
The key to shrinkage control is “consistency.”
Oven Temperature Control: Errors must be kept within ±2°C.
Cycle Time: The duration each figure spends in the mold is kept identical to prevent shrinkage variances caused by different heating times.
4. Comprehensive Coverage of Setting Jigs & Fixtures
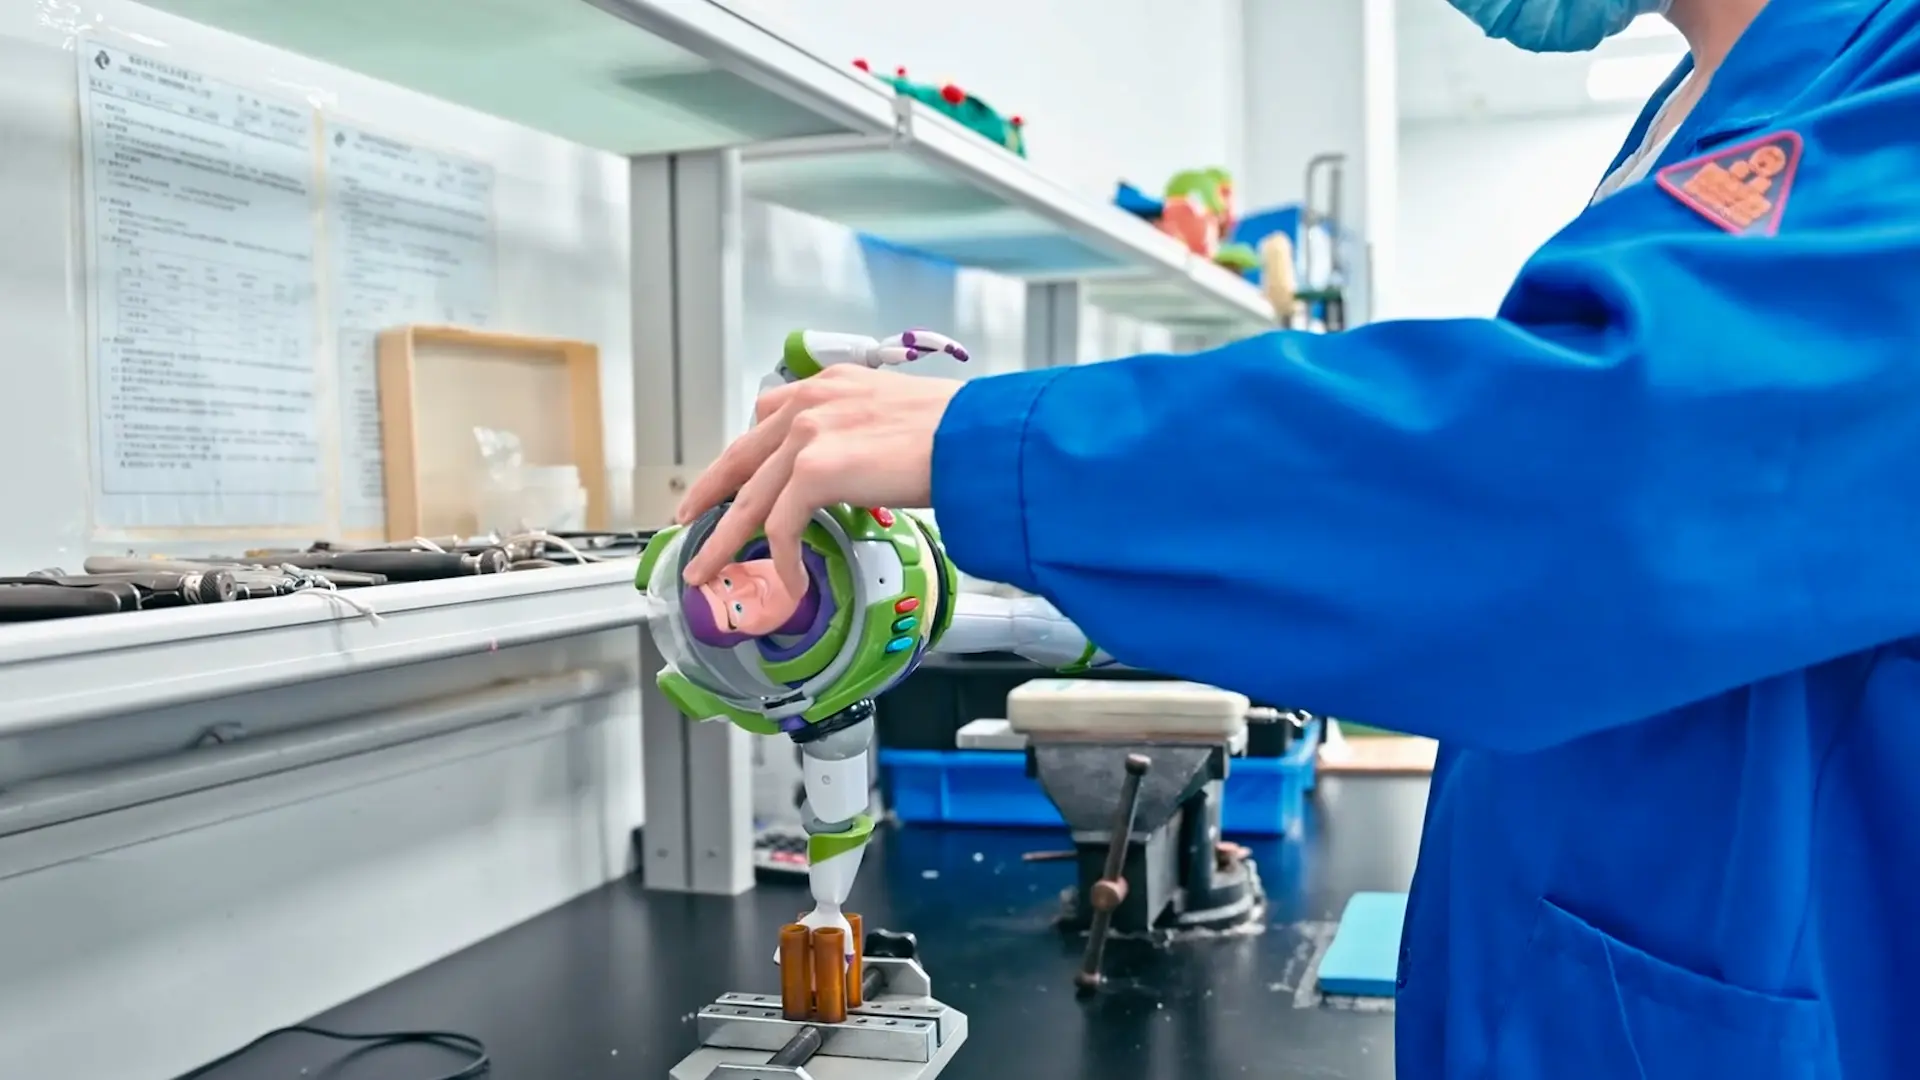
For all parts requiring assembly, MIHOX develops matching cooling setting jigs simultaneously with mass production molds.
Immediately after leaving the mold, assembly ports are fitted onto standard-sized rigid plugs.
Forced cooling is performed under this constraint, allowing the material to solidify and reorganize its molecular chains within the set dimensions, completely curing the “oval interface” problem.
Part 4: Technical Data Reference Table
To provide your design team with an intuitive reference, we have summarized technical parameters for different scenarios:
| Technical Indicator | Hard Vinyl (Shore A 85+) | Standard Medium (Shore A 75-80) | Soft Accessories (Shore A 65-) |
|---|---|---|---|
| Typical Shrinkage Rate | 1.6% – 1.8% | 1.9% – 2.2% | 2.3% – 2.8% |
| Recommended Wall Thickness | 2.0mm – 2.5mm | 2.5mm – 3.5mm | 3.0mm – 4.0mm |
| Gap Control Standard | < 0.15mm | < 0.25mm | < 0.40mm |
| Mold Compensation Coefficient | 1.017 | 1.021 | 1.026 |
| Core Setting Method | Forced Air + Inner Plug | Natural Cool + Outer Clamp | Water Cool + Full Mold Fixture |
Swipe horizontally to view full table ↔
Part 5: Five Practical “Pitfall Avoidance” Tips for Brand Owners
If you want mass production with both soft and hard textures, please inform the factory in advance. This requires developing two sets of molds with different compensation coefficients.
When designing your IP, try to place parting lines at collars, belts, clothing edges, or natural body folds. Even if a physical gap occurs, it will be perceived as a structural shadow.
Mating two perfectly flat surfaces is extremely difficult in rotocasting. We recommend using curved surfaces or stepped interfaces.
The PP sample must be a rotocast sample, not a 3D-printed resin sample. Only a rotocast sample reflects the true shrinkage effect.
When auditing suppliers, observe if they have setting jigs on their assembly lines. Factories without jigs cannot guarantee stable assembly quality at scale.
Part 6: FAQ – Frequently Asked Questions
Q1: Why do some figures in the same batch have larger gaps than others?
Q2: Do environmental certifications (e.g., Non-Phthalate, REACH) affect shrinkage?
Q3: If mass production is already finished and gaps are too large, can it be fixed?
Q4: Does this shrinkage control method significantly increase customization costs?
Q5: How does MIHOX handle uneven shrinkage in irregular parts (like clouds or flames)?
Conclusion
In vinyl toy manufacturing, shrinkage is not the “enemy”—it is a “variable.” The value of a professional factory like MIHOX lies in transforming this uncertain variable into a deterministic technical parameter through deep industry experience and standardized engineering processes.
Whether you are a brand new to the designer toy world or an industry veteran with strict quality requirements, understanding and respecting the physical nature of the process and choosing a supplier with deep technical roots is the only shortcut to ensuring your IP is realized perfectly.