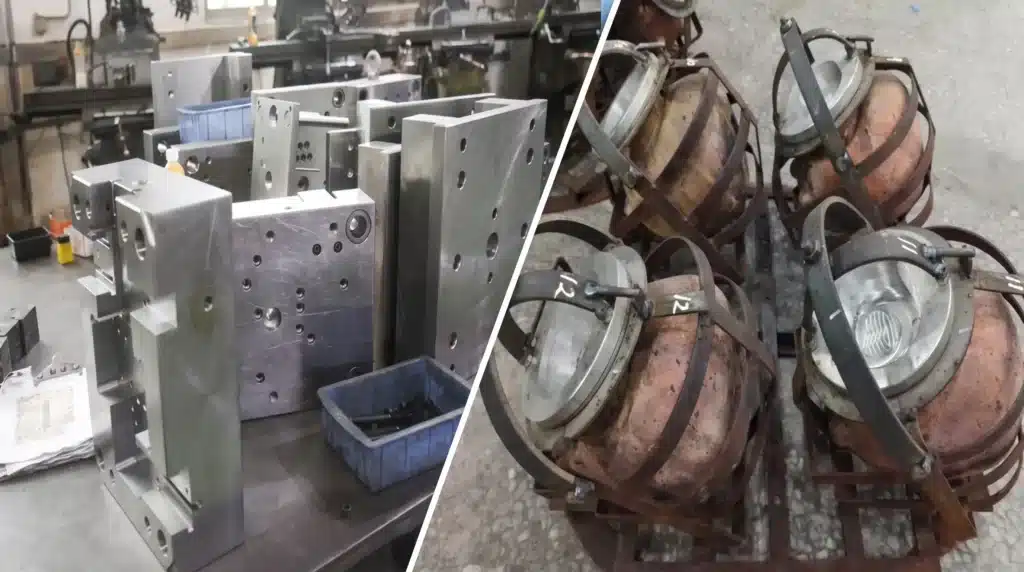
Quick answer: a copper slush mold and a steel injection mold are not two prices for the same tool. They are two tooling systems with different replacement logic, tolerance bands and failure modes. The correct decision is based on part architecture, total cost of ownership and the cost of being wrong — not the headline mold quote.
Most buyers compare molds on one line: price. That is where the decision starts going wrong.
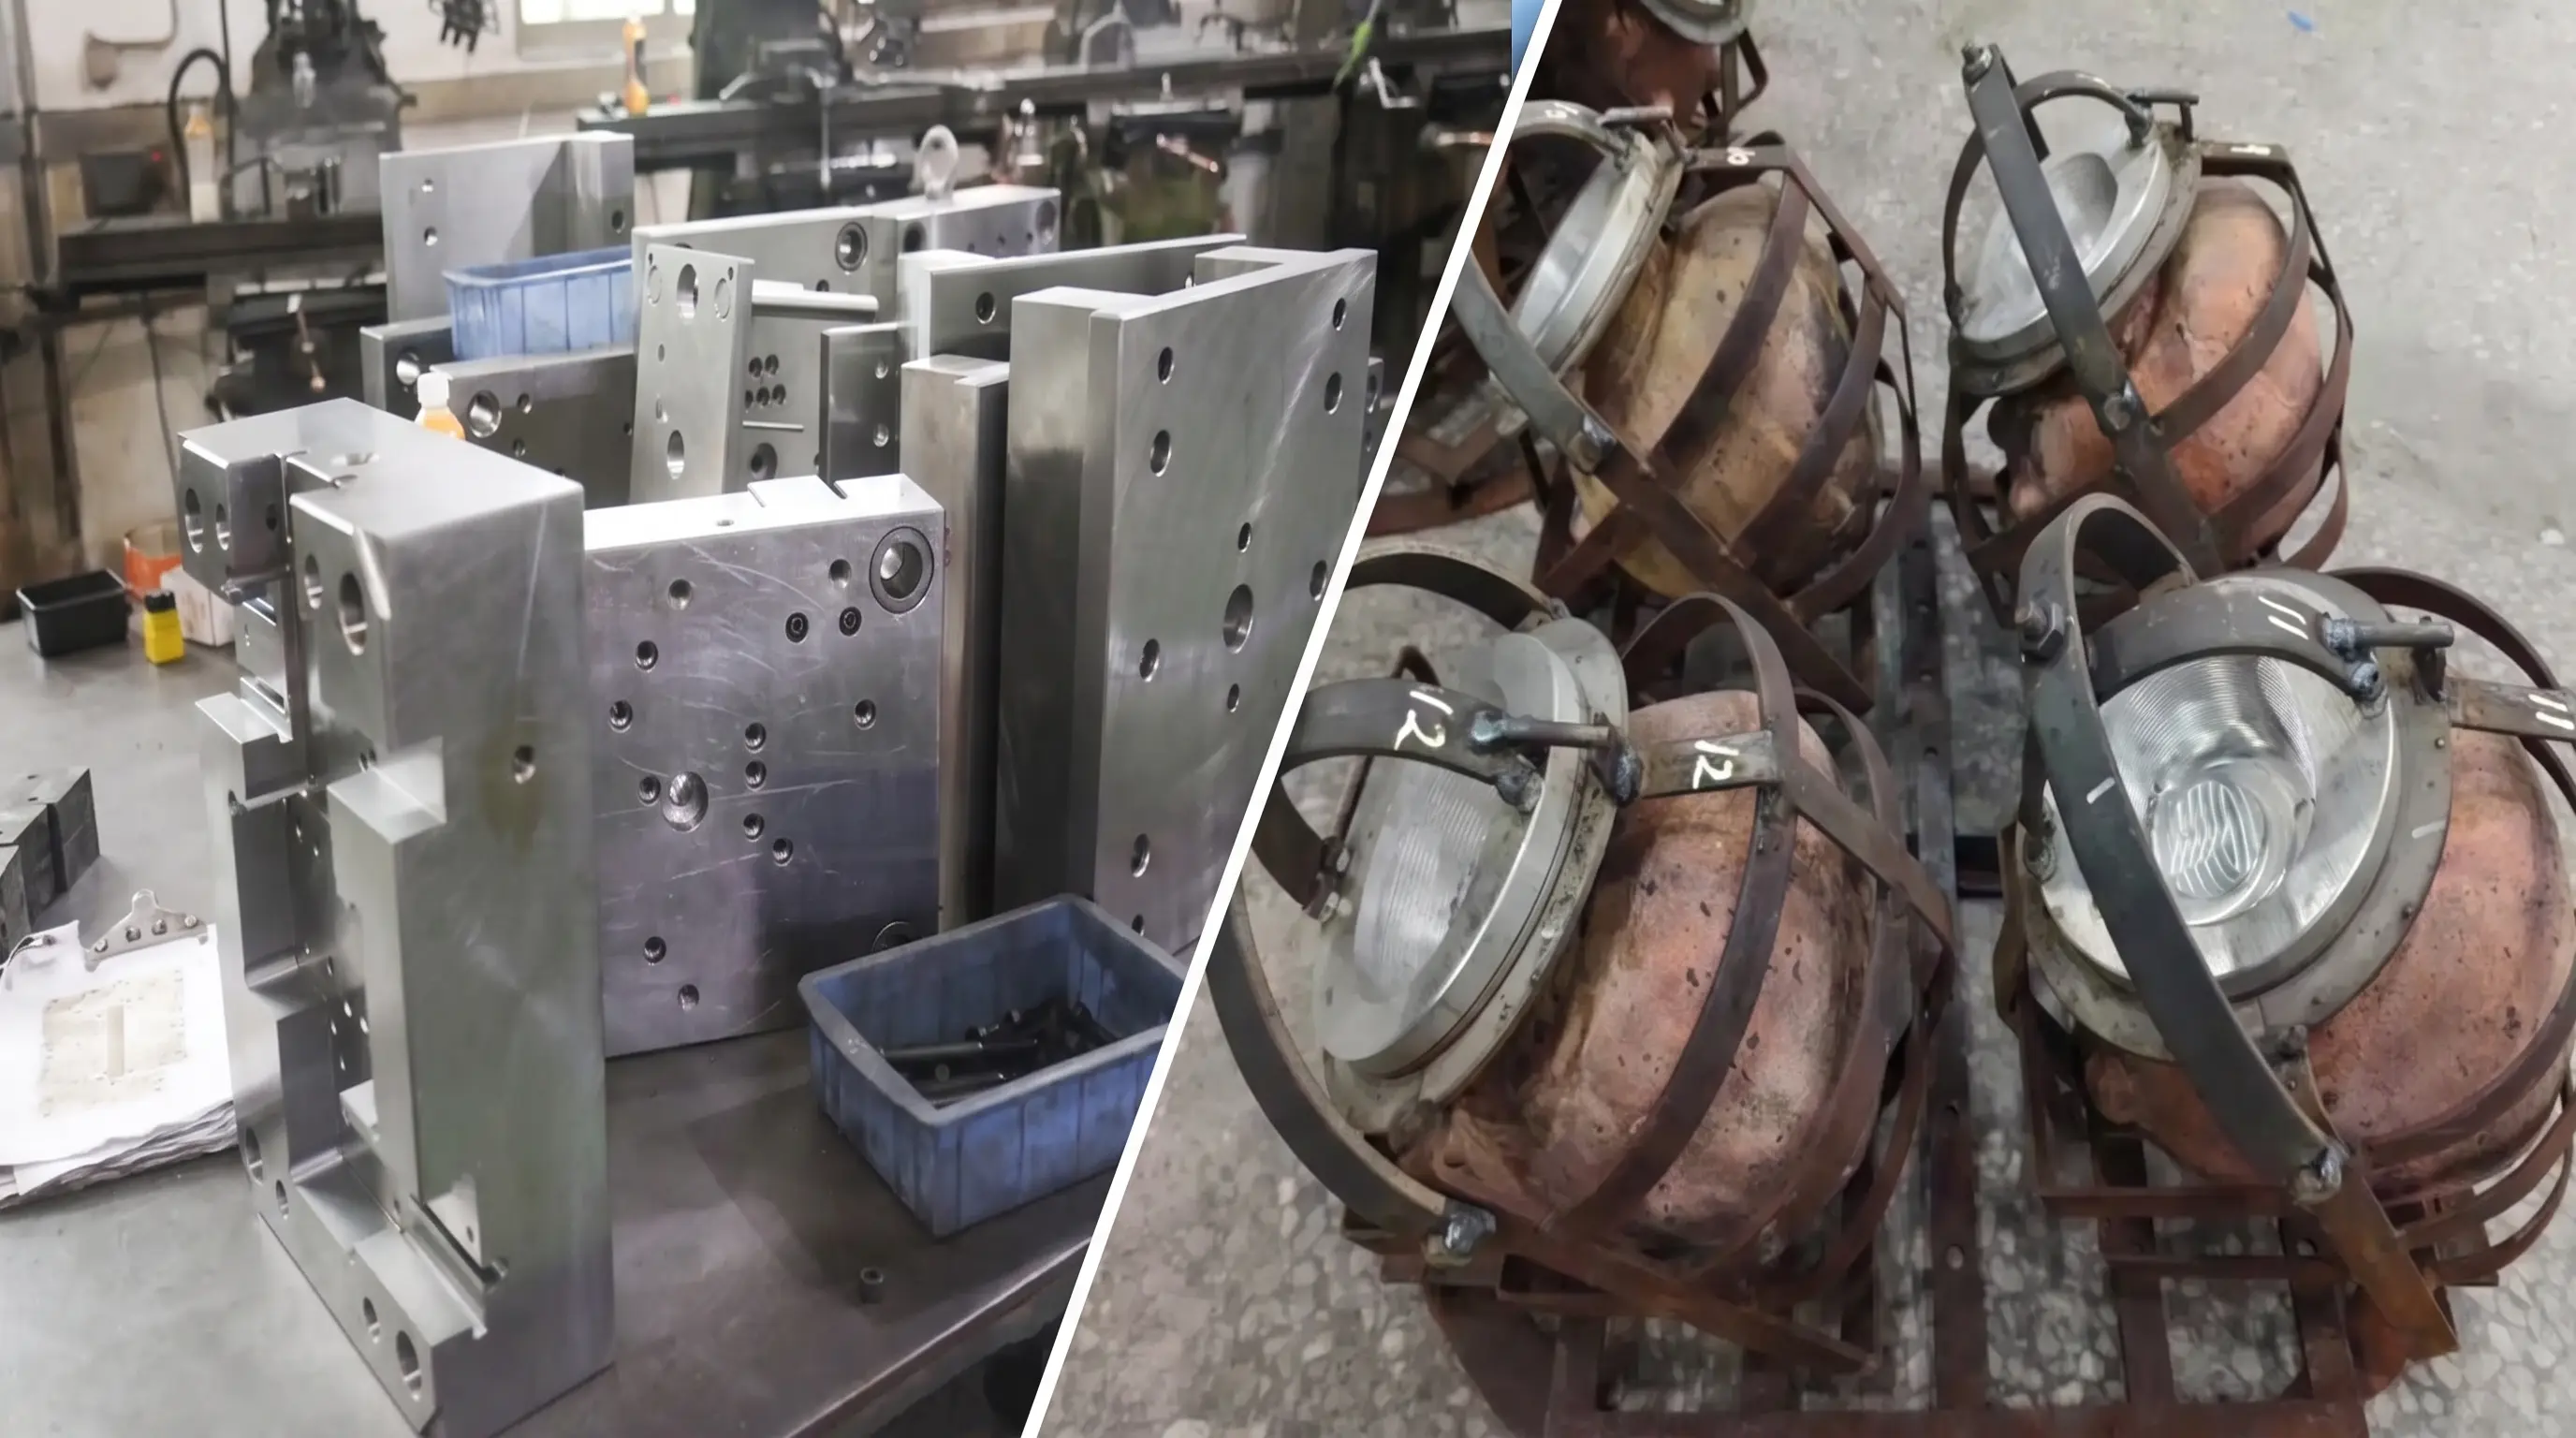
A copper mold is a thin electroformed shell used to make a hollow vinyl skin. A steel mold is a machined tool used to hold rigid geometry across a long injection run. One is closer to a consumable; the other is closer to a capital asset. They fail differently, they change differently, and they carry different commercial risk.
This guide is written for the buyer who has to defend the decision internally — not just pick the lower quote.
The two tooling systems, in operational terms
Copper slush tooling
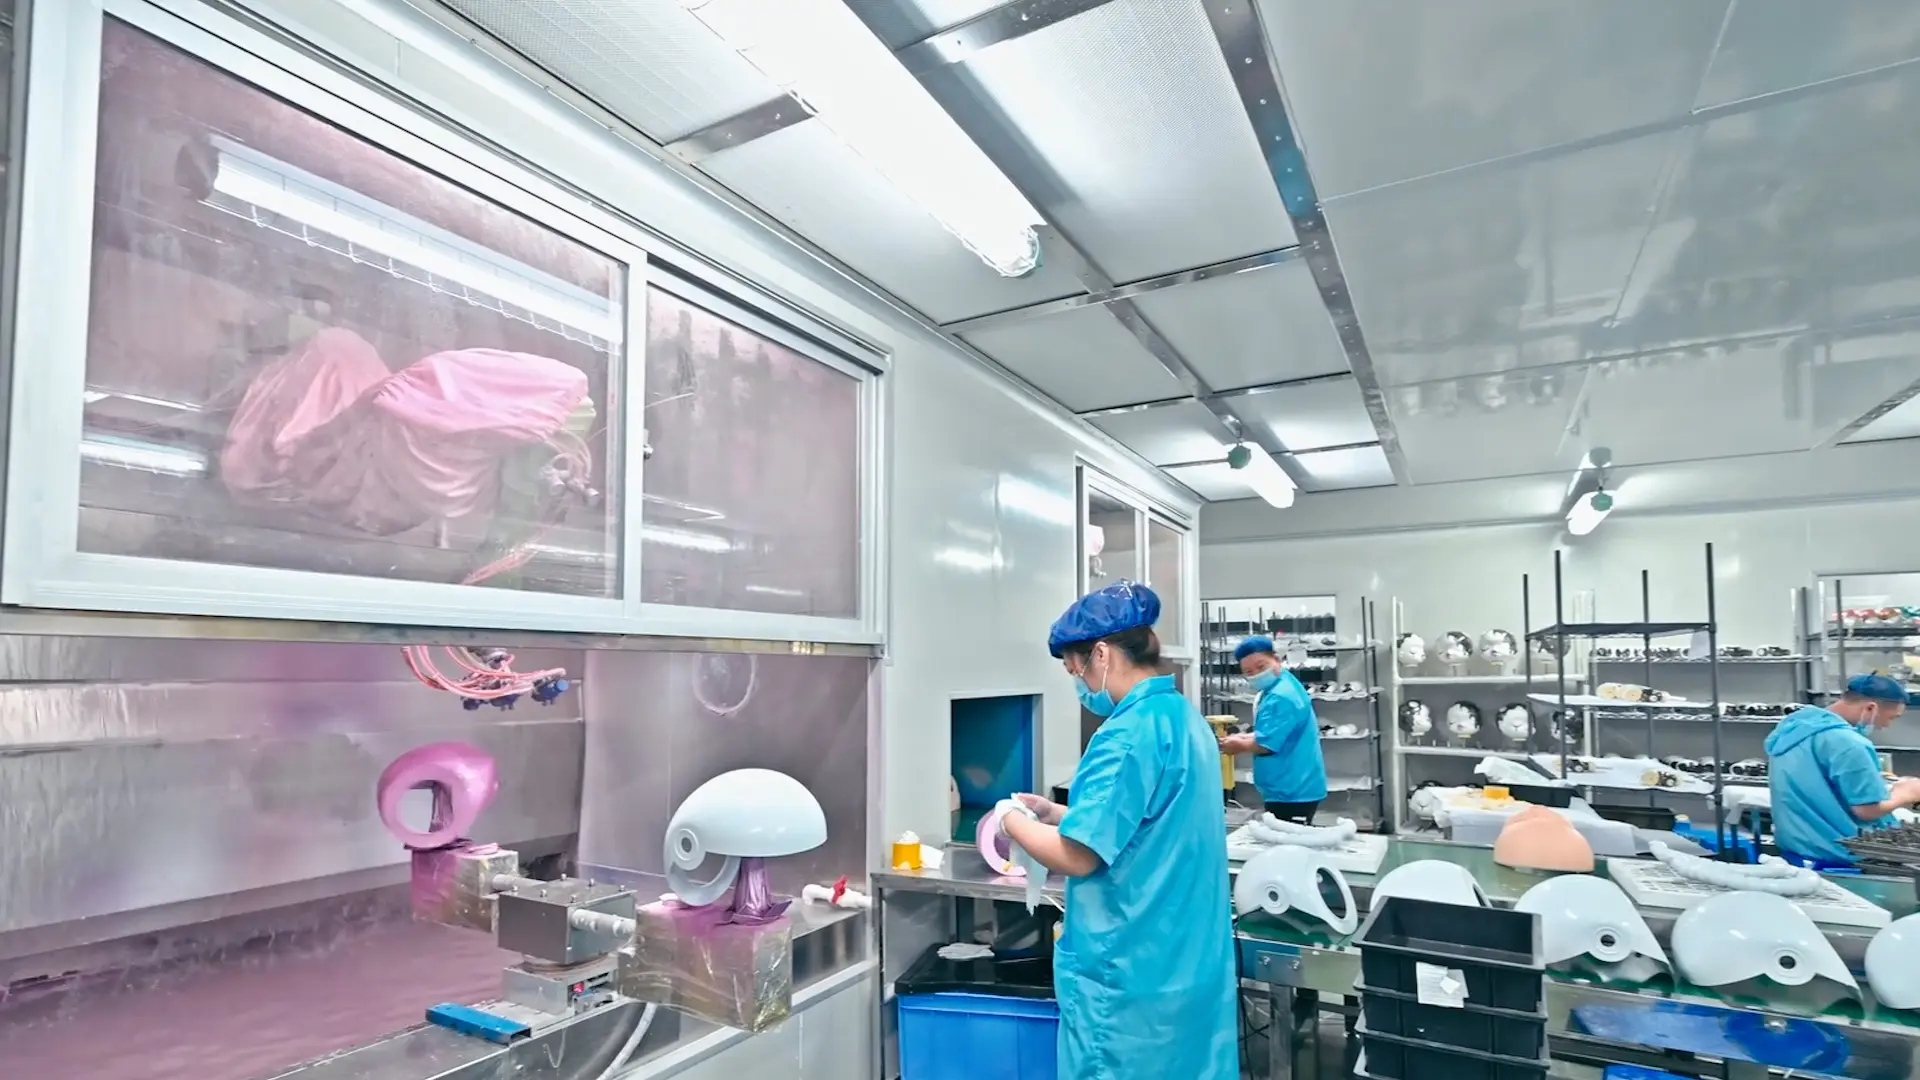
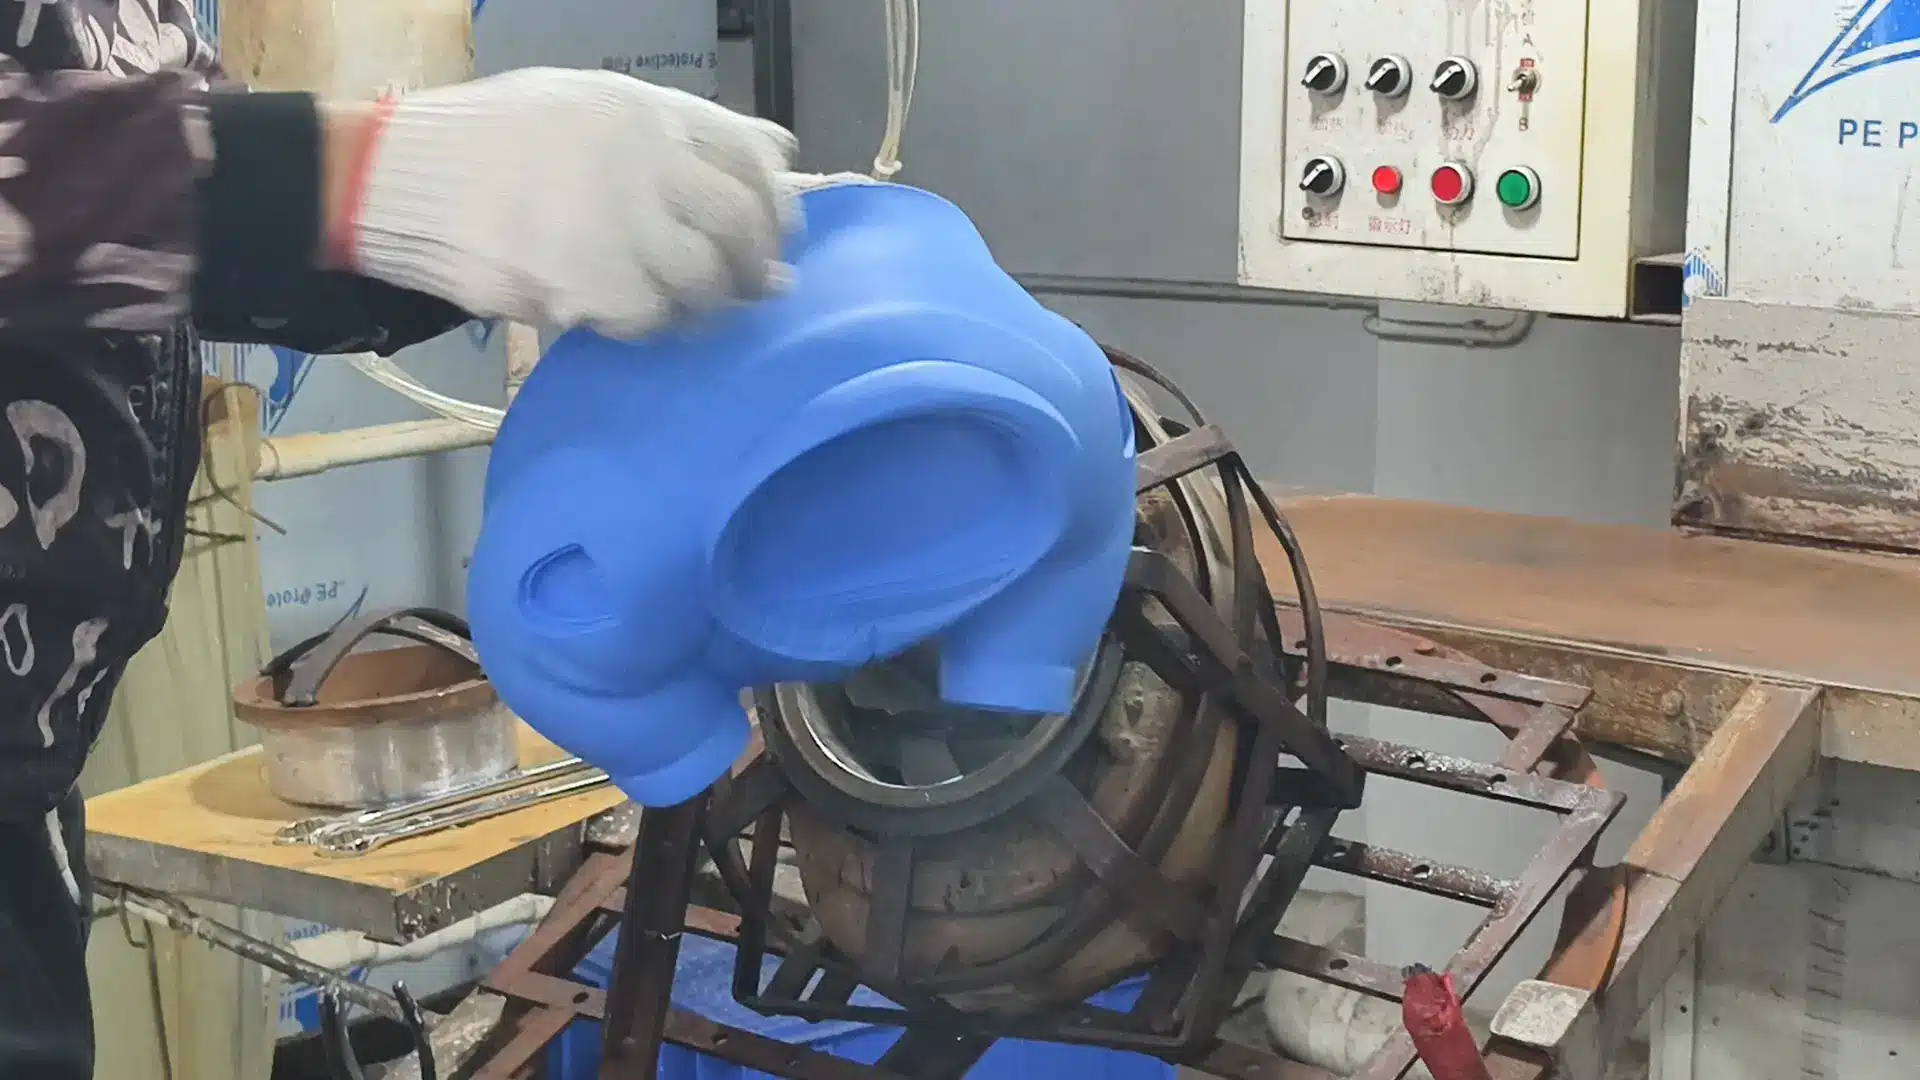
A copper mold is built around a master pattern, usually through a silicone mold and a wax duplicate. The wax is made conductive, copper is deposited in a plating bath, and the wax is melted out. The result is a hollow copper shell.
That shell is used with liquid PVC compound in a slush or rotocast process. The material coats the inside of the heated mold, then cools into a skin. The part is removed by hand.
The important point is not “copper is cheaper.” The important point is that the mold is a shell. It reproduces an organic master very well, but its opening rim and fine texture are consumable. A serious copper program keeps the master pattern and plans for a replacement shell.
Steel injection tooling
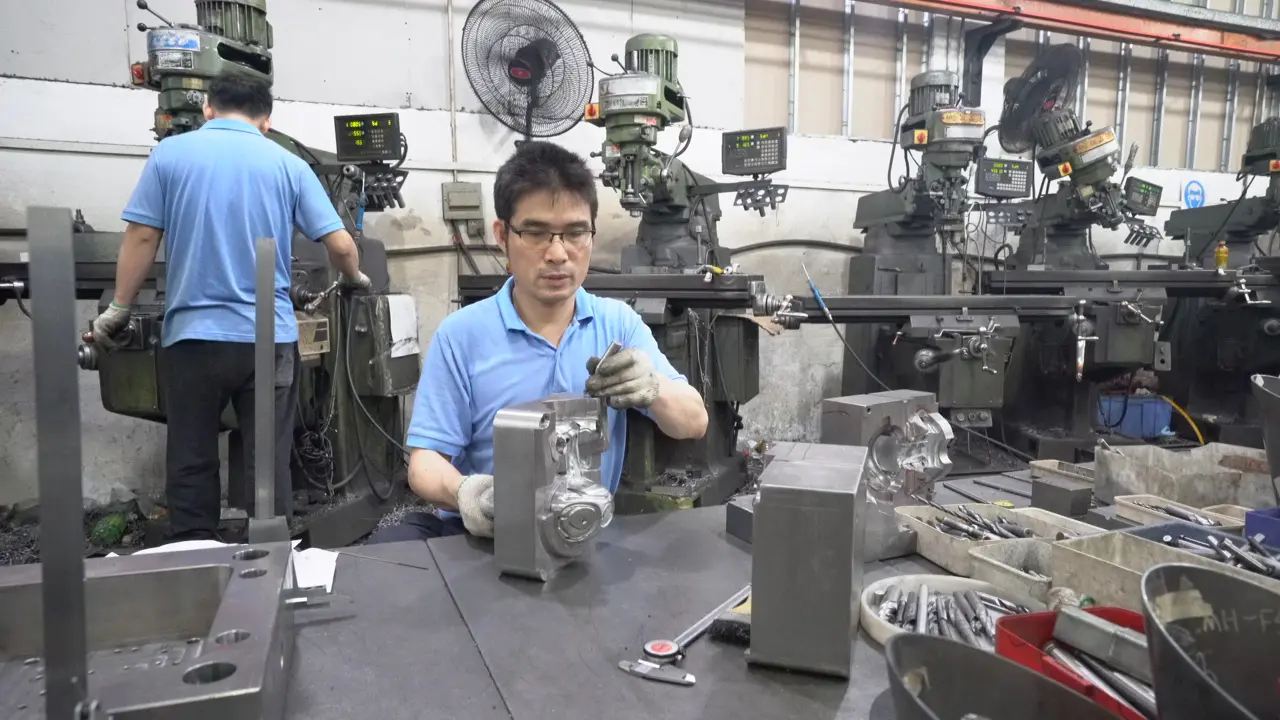
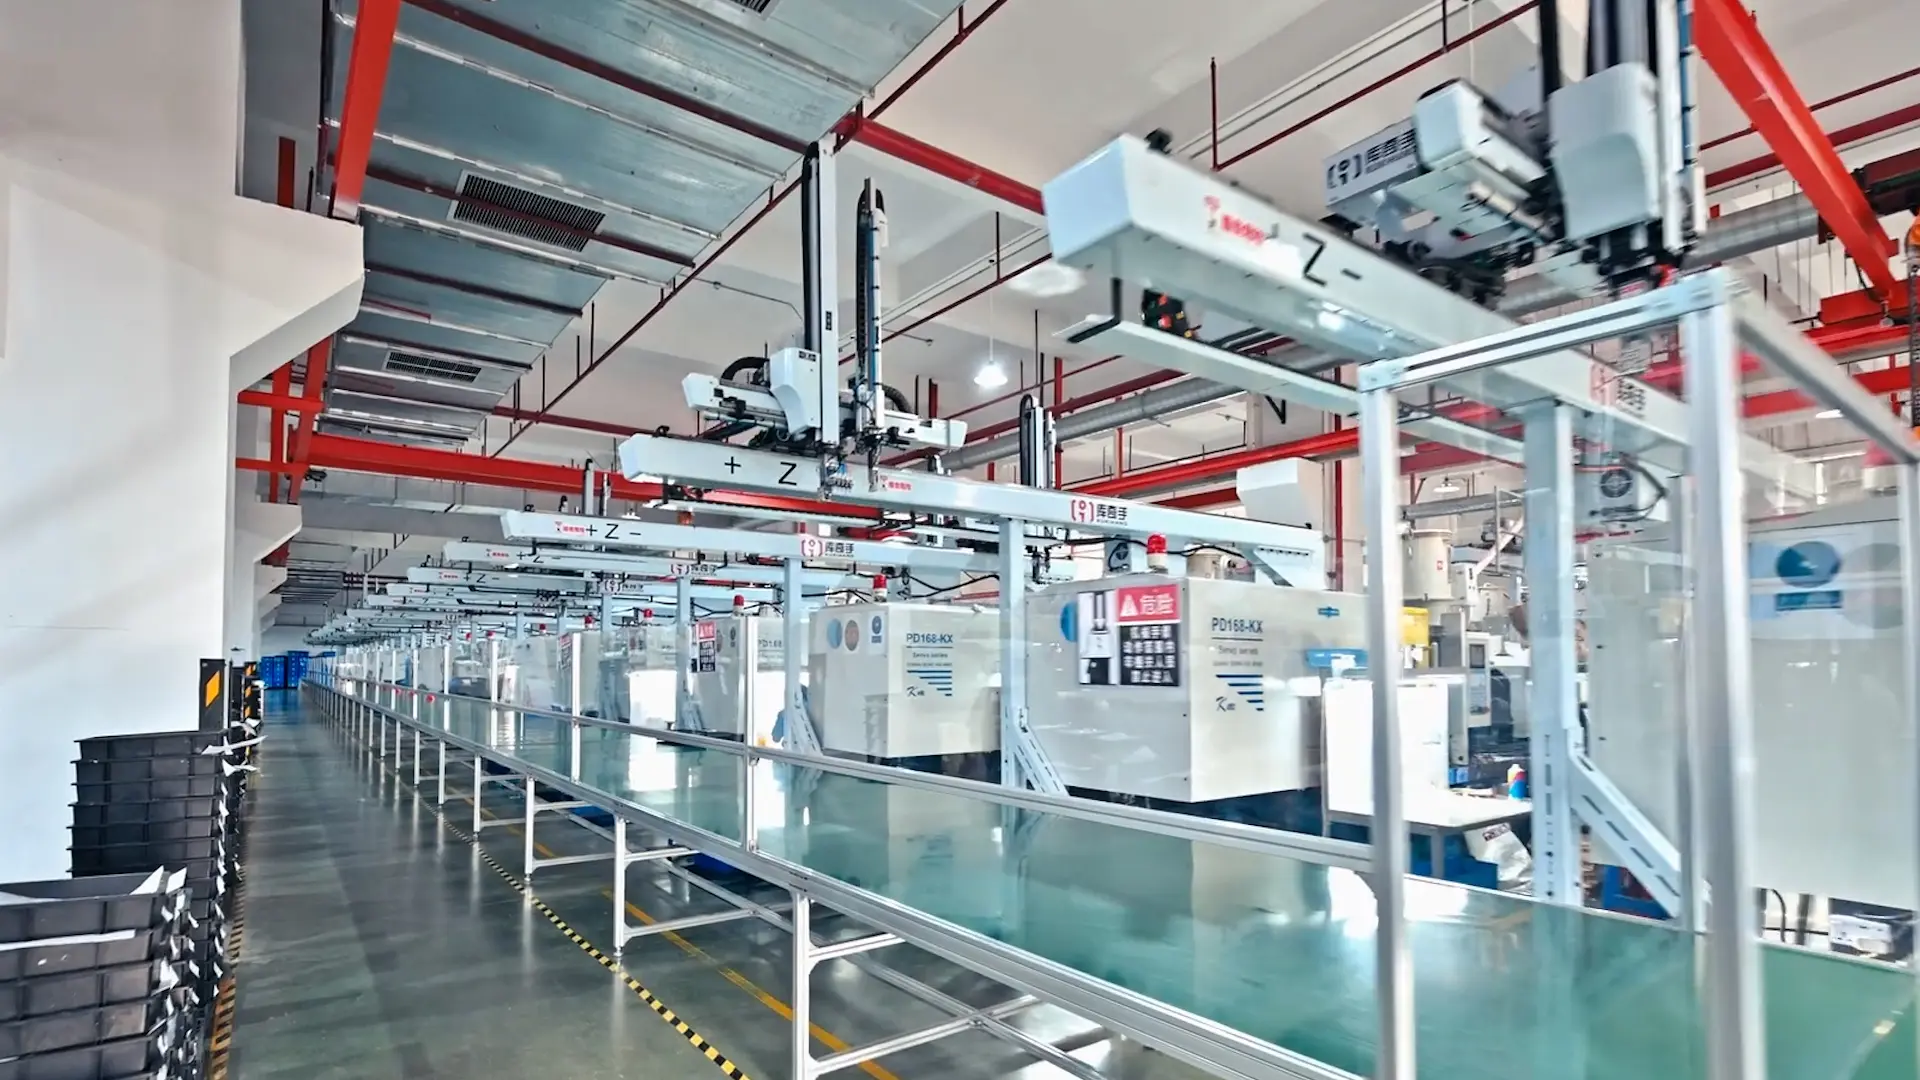
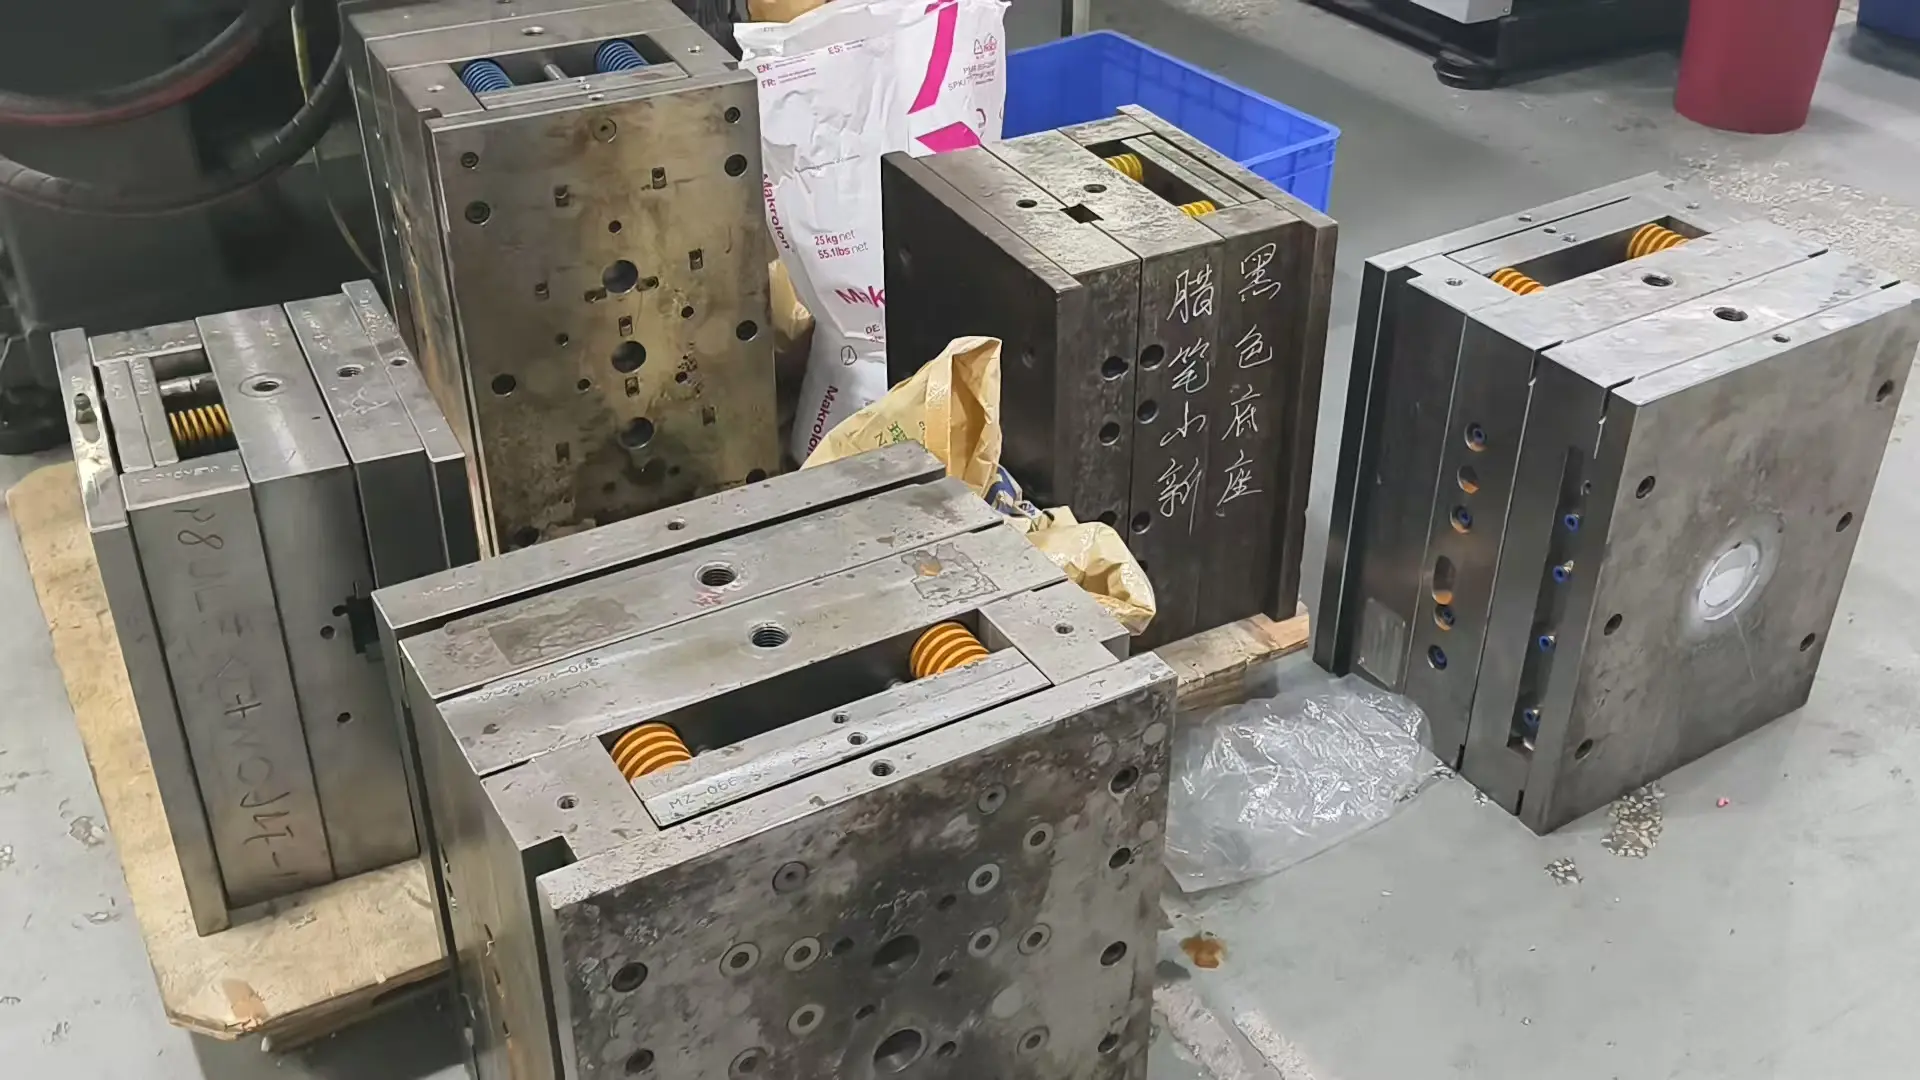
A steel mold is machined from tool steel. The cavity and core are cut by CNC, EDM and related processes, then fitted, polished and tested. It runs in an injection molding machine under pressure.
Steel tooling is a capital tool. It is designed to hold geometry over a long run, and it can often be maintained, repaired or modified. That does not make it permanent, but it changes the accounting: the mold is amortized across volume, and the buyer should plan maintenance and spare inserts.
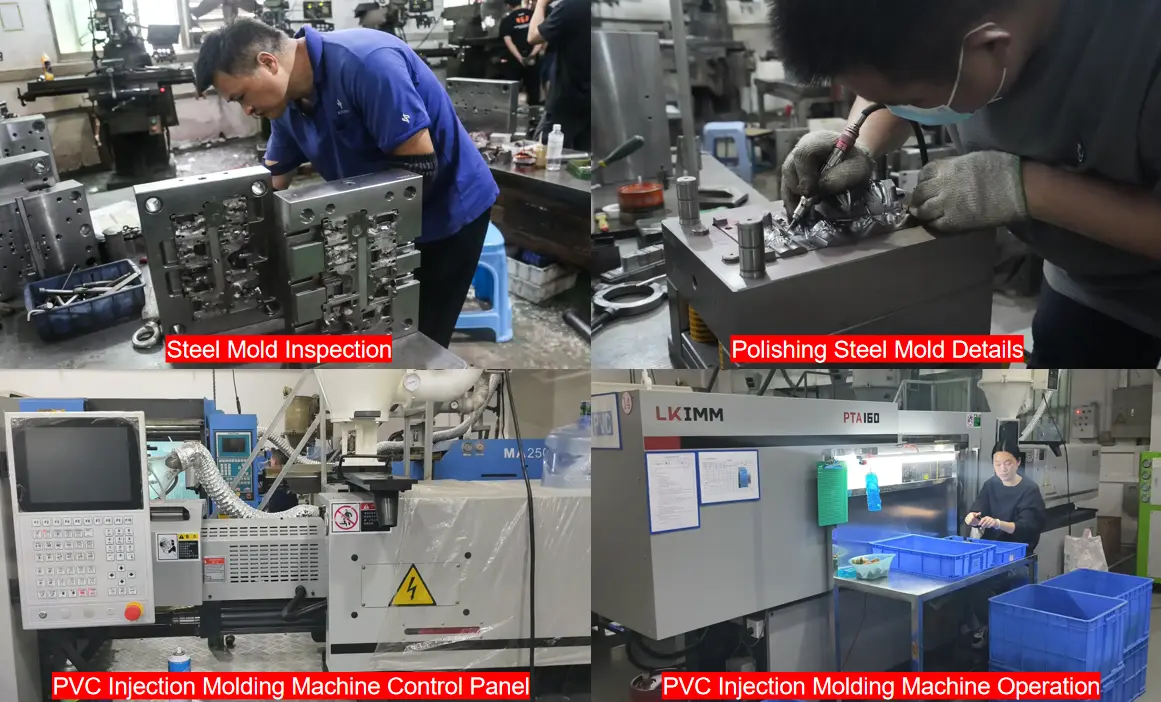
If you need the process detail behind each route, see soft vinyl copper mold manufacturing and steel injection mold manufacturing.
The comparison that matters
| Decision layer | Copper slush tooling | Steel injection tooling |
|---|---|---|
| Part architecture | Hollow skin; organic shell | Solid or rigid part; assembly features |
| Tooling economics | Lower entry cost; replacement expected | Higher entry cost; amortized over volume |
| Life model | Shell wear; plan a replacement | Tool wear; plan maintenance and inserts |
| Tolerance | Wider band; shrinkage and hand demolding | Tighter band; better for joints and snap fits |
| Surface | Organic texture, soft folds, hand-sculpted detail | Crisp edges, flat planes, sharp graphics |
| Material | Liquid PVC compound, some rotocast materials | ABS, PVC, PC, POM, acrylic and other thermoplastics |
| Change model | New master or new shell | Weld, insert or re-machine where possible |
| Best fit | Limited vinyl drops, hollow character toys | Mass rigid parts, articulated figures, functional toys |
Mold life and tolerance are project-specific. Do not accept a blanket number from a supplier without the part drawing, material, cavity count and maintenance plan.
The total cost of ownership model buyers should use
The real comparison is not:
Mold A price vs Mold B price.
It is:
Cost per saleable unit over the planned program, including the cost of the mold’s failure mode.
A practical model is:
TCO per 1,000 saleable units =
- tooling cost;
- replacement or maintenance reserve;
- trial and sample cost;
- expected rework and scrap;
- assembly adjustment cost;
- delay or obsolescence cost;
- divided by 1,000 saleable units.
This is where copper and steel separate.
A copper program should include a replacement reserve. If the shell is planned to lose detail or rim condition before the program ends, the replacement is not a surprise; it is a line in the budget. The reserve is the replacement shell quote multiplied by the number of replacements you expect to need.
A steel program should include a maintenance and insert reserve. The mold may last a long time, but sliders, inserts, ejection and cooling circuits still wear. The reserve is the planned repair and spare-part budget across the program.
The rest of the model is often ignored:
- Scrap: a wider tolerance band can create more assembly rejects, especially at a painted interface.
- Rework: reaming, shimming, trimming or repainting a joint can cost more than the mold difference.
- Delay: a mold that misses the launch window can cost more than the tooling itself.
- Obsolescence: a mold built for a design that changes before launch is a stranded asset.
For the cost structure around tooling, see art toy tooling cost explained and collectible production cost factors.
Five layers of the mold decision
Layer 1: Part architecture
Start with the part, not the material.
- Is it a hollow skin or a solid body?
- Does it need a snap fit, a screw boss, a hinge or a ball joint?
- Are there undercuts, thin walls, deep ribs or optical surfaces?
- Does the part carry load, or is it primarily visual?
A hollow vinyl skin and a rigid articulated body are different architectures. A copper shell is good at one; a steel tool is good at the other. If the design mixes both, that is a hybrid conversation, not a single-mold conversation.
Layer 2: Material and process window
Copper slush tooling runs liquid PVC compound. Steel injection tooling runs thermoplastics under pressure. The material decision is not only “soft vs hard.” It affects:
- wall thickness and part weight;
- shrinkage and warpage;
- surface finish and paint adhesion;
- clearance and joint feel;
- drop performance and packing protection.
If the design needs a transparent part, a stiff weapon, a battery housing or a structural frame, the material window usually points to steel. If it needs a hollow, soft-touch vinyl skin, copper is the natural route.
Use the material pages as a reference: PVC and ABS material selection and vinyl material guide.
Layer 3: Tolerance stack and interface
This is where many projects fail.
A mold can be “in tolerance” and the assembly can still fail because the tolerance stack was never reviewed. A soft vinyl body shrinks differently from a rigid ABS joint. Paint adds thickness. The joint clearance has to absorb all of it.
For a hybrid figure, define:
- the datum surface;
- the nominal clearance at the joint;
- the paint build-up allowance;
- the acceptable push/pull force;
- the inspection method for the assembled part, not only the molded part.
If the supplier quotes a mold without asking for the assembly stack, the quote is incomplete.
Layer 4: Volume, life and replacement
A copper shell is not a permanent tool. A steel mold is not immortal either.
The right question is:
How many saleable units does this program need before the tool’s failure mode becomes a business problem?
For copper, plan the replacement shell before the detail or rim condition degrades. For steel, plan maintenance and spare inserts before the wear affects the part. The volume decision is not only “how many units”; it is “how many units before the tool needs intervention.”
Layer 5: Change and commercial terms
Design changes are part of tooling economics.
A copper change often means a new master or a new shell. That can be efficient for a small art toy, but expensive if the design is still moving. A steel change may be a weld, insert or re-machine, but only if the change fits the mold structure. A major geometry change can still require a new tool.
Before the purchase order, agree:
- who owns the mold and the master pattern;
- who owns the 3D file and the tooling data;
- how design changes are quoted;
- how the mold is stored and maintained;
- what happens if the program ends early;
- whether the tool can be transferred.
For the commercial side, see MOQ and volume negotiation and quality control process.
The failure modes buyers should ask about
Copper shell failure modes
- texture loss after repeated heat cycles;
- opening rim deformation;
- uneven shell thickness;
- flash at the parting line;
- shrinkage variation between shots;
- paint adhesion problems on a contaminated skin;
- difficulty reproducing a sharp undercut.
Ask the supplier how shell thickness is checked, how the rim is maintained and when a replacement is recommended. A supplier who cannot describe the wear limit is guessing.
Steel mold failure modes
- short shots from a poor gate or vent;
- sink and warpage from cooling imbalance;
- flash from insufficient clamp or worn parting surfaces;
- ejection marks and drag marks;
- slider wear and galling;
- cooling-channel scale and cycle drift;
- steel-safe changes that were not planned.
Ask for the T0/T1 sample plan, the cooling and ejection review, and the steel-safe report. A “we will fix it at trial” answer is not a plan.
The hybrid decision: one product, two tooling systems
Many high-end collectibles use a soft vinyl body with rigid ABS or POM parts. That is often the right architecture, but it is not two independent mold purchases.
A hybrid program has to control:
- the shrink difference between vinyl and rigid plastic;
- the joint clearance after paint;
- the datum used for assembly;
- the inspection method for the assembled figure;
- the replacement plan for the copper shell and the steel inserts.
The common mistake is to design the vinyl body and the rigid joint separately, then discover at assembly that the interface is wrong. The mold decisions can each be correct and the product can still fail.
How to normalize two mold quotes
Two quotes are comparable only when the scope is the same. Build a line-by-line comparison:
- cavity count and spare cavities;
- steel grade or copper shell build;
- slider, lifter and undercut scope;
- surface finish and texture;
- T0/T1 sample rounds;
- spare inserts and wear parts;
- maintenance and storage terms;
- expected life and replacement plan;
- design-change rate;
- ownership and transfer terms.
A low quote with fewer cavities, a simpler finish or no trial round is not a cheaper version of the same tool. It is a different tool with a different risk profile.
Three project profiles
Limited art toy drop
A small run of a hollow vinyl character with an organic sculpt and a short launch window usually fits copper slush tooling. The lower entry cost and the hollow skin are the advantages. The buyer should still budget for a replacement shell and confirm the paint and demolding plan.
Large blind-box or retail line
A large run of rigid parts with repeatable color, snap fits and retail packing usually fits steel injection tooling. The tooling cost is higher, but it can be amortized across volume. The buyer should ask for the cooling, ejection and steel-safe plan, not only the mold price.
Articulated collectible
An articulated figure with a soft vinyl head and rigid joints often fits a hybrid route. The key is not the mold list; it is the interface. Review the shrink difference, joint clearance and assembly inspection before approving either tool.
A simple decision scorecard
Score each item from 1 to 5, then weight the result. This is more useful than a generic “copper vs steel” table because it forces the team to state the real priority.
| Question | Weight | What a high score means |
|---|---|---|
| Hollow skin is essential | High | Copper route |
| Tight joint or snap fit is essential | High | Steel route |
| Organic surface is the selling point | Medium | Copper route |
| Crisp geometry is the selling point | Medium | Steel route |
| Volume is high and repeat demand is expected | High | Steel or hybrid |
| Launch is small and demand is unproven | High | Copper or hybrid |
| Design may change after the first sample | Medium | Check change model before choosing |
If the scorecard gives no clear answer, the product probably needs a hybrid review — not another generic comparison.
How MIHOX reviews the decision
The review starts with the 3D file and the assembly, not a preferred mold type.
- Check the part structure, wall, undercuts and assembly.
- Confirm the material and surface requirement.
- Build the tolerance stack for the assembled product.
- Estimate volume, tool life and replacement reserve.
- Select copper, steel or a hybrid route.
- Normalize the quote scope and sample plan.
- Confirm the first-article sample before mass production.
MIHOX plans both steel injection tooling and copper slush tooling for soft vinyl, so the recommendation can follow the product rather than a single in-house process. For the factory side, see Mi-Ho factory.
Frequently asked questions
What is the main difference between steel and copper molds?
How long does a copper mold last?
Can a steel mold make hollow soft vinyl?
Can one toy use both mold types?
Which mold is cheaper?
What should I ask for before approving a mold?
Next step: send the 3D file, target quantity, material direction and assembly tolerance.
MIHOX will review whether the part suits copper slush tooling, steel injection tooling or a hybrid route, and confirm the next sample step.